





Explore our CE & ATEX certified high-torque, slip ring, wound rotor, and high-voltage asynchronous motors tailored for hazardous environments, mining, heavy cranes, and oil & gas applications.
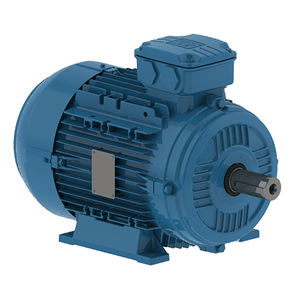

In high-risk industrial environments such as offshore oil platforms, chemical processing plants, underground coal mines, and grain handling facilities, electrical equipment operates under the continuous threat of explosive gas mixtures, volatile vapors, or combustible dust clouds. As a premier global supplier and exporter with over 128 years of rotating equipment heritage (tracing roots to TDC Parsons Peebles and historical manufacturing centers in Edinburgh and Birmingham), our engineering division specializes in the design, manufacture, and rigorous validation of CE certified explosion-proof electric motors.
Compliance with European Union directives—specifically the ATEX Directive 2014/34/EU, the Machinery Directive 2006/42/EC, and the Low Voltage Directive 2014/35/EU—is not merely a regulatory prerequisite; it represents the ultimate operational safeguard for personnel and plant infrastructure. A true explosion-proof motor (whether classified under Flameproof Ex d, Pressurized Ex p, or Increased Safety Ex e / Ex ec) must possess the structural integrity to withstand internal explosions without allowing flames or thermal hot spots to ignite the surrounding hazardous atmosphere.
Engineers and procurement specialists must carefully match the motor protection concept with the specific hazardous zone classification (Zone 1, Zone 2 for gases; Zone 21, Zone 22 for dusts):
Technical comparison of explosion-proof protection standards to streamline procurement and engineering specifications for global EPC projects.
| Protection Code | Design Principle | ATEX / IECEx Zone | Typical Power Range | Key Advantage |
|---|---|---|---|---|
| Ex d / Ex db | Flameproof Enclosure | Zone 1, Zone 2 (Gas) | 0.75 kW - 1,500 kW | Contains internal explosions; no purging control system required. |
| Ex p / Ex px | Pressurized Enclosure | Zone 1, Zone 2 (Gas) | 250 kW - 25,000 kW+ | Ideal for High Voltage (3.3kV to 13.8kV) heavy industrial drives. |
| Ex e / Ex ec | Increased Safety / Non-Sparking | Zone 2 (Gas) | 0.55 kW - 5,000 kW | Highly cost-effective, energy efficient with minimal thermal stress. |
| Ex tb / Ex tc | Dust Ignition Proof | Zone 21, Zone 22 (Dust) | 0.37 kW - 2,000 kW | High IP66 ingress sealing; prevents combustible dust accumulation. |
| CACA / CACW | Air-Air / Air-Water Cooling | Zone 1 & 2 Custom MV/HV | 500 kW - 15,000 kW | Customized closed-loop heat exchangers for harsh marine/desert climates. |
Fully compliant with EU Directives. Certified by accredited notified bodies like SGS Baseefa, ensuring seamless international deployment across EU and global territories.
100% mechanically and electrically interchangeable replacement engineering. Eliminates costly civil modifications, pipework changes, or cable trench redesigns.
Engineered for ambient temperatures ranging from sub-zero arctic conditions (-50°C) to extreme desert ambient levels (+60°C) with specialized anti-corrosion marine paint.
State-of-the-art testing facility supporting No-Load, Full Load, Back-to-Back, and Core Flux Testing up to 13.8 kV, guaranteeing verified performance before dispatch.
Customized insulation systems rated for high dV/dt voltage spikes from inverter drives, paired with insulated bearings to stop harmful shaft currents.
Every manufacturing step—from copper rotor bar insertion to final VPI curing—is governed by strict quality management protocols accredited under international standards.
As global industries double down on energy efficiency and carbon reduction while maintaining stringent plant safety, procurement directors and facility managers face a changing technological landscape. Understanding these key trends is critical to making future-proof capital expenditure (CAPEX) decisions:
Historically, explosion-proof motors traded a degree of electrical efficiency for robust flameproof structural integrity. However, recent regulatory mandates across Europe, North America, and Asia now enforce IE3 (Premium) and IE4 (Super Premium) efficiency levels even for Ex-rated motors. Modern design utilizes ultra-low loss silicon electrical steel, optimized stator slot filling, and precision-balanced copper rotors to minimize heat generation, directly extending insulation life while lowering total cost of ownership (TCO).
Unplanned downtime in a chemical refinery or offshore platform can cost hundreds of thousands of dollars per hour. The integration of intrinsic safety certified (Ex i) IoT sensors directly onto motor frames allows continuous real-time monitoring of tri-axial vibration, bearing temperature, winding insulation health, and acoustic signatures. Wireless predictive analytics enable plant operators to transition from reactive repairs to condition-based maintenance.
With industrial process units expanding production capacities, the demand for mega-watt class high-voltage drives (3.3kV, 6.6kV, 10kV, 11kV, 13.8kV) has surged. For motor ratings exceeding 2,000 kW, traditional cast Ex d housings become excessively heavy and cumbersome. Procurement is rapidly shifting toward custom-engineered Ex p (Pressurized) systems fitted with automated purging control units, offering lightweight, highly accessible, and ultra-reliable operations in gas-hazardous areas.
The global transition to green hydrogen energy requires electrical equipment certified for Gas Group IIC (which includes hydrogen and acetylene), characterized by extremely small flame gap paths and high ignition susceptibility. Future-ready procurement strategies require specifying motors with verified IIC flame-path dimensions, anti-static external cooling fans, and non-sparking terminal connections.
With an engineering legacy spanning over a century, our brand stands shoulder-to-shoulder with global industry pioneers like WEG, Parsons Peebles, ABB, and Siemens. Operating out of premier manufacturing and testing workshops located in the UK (including Rosyth Royal Dockyard, Fife, and Birmingham), we combine historical engineering expertise with cutting-edge manufacturing technology.
Confidence in hazardous area equipment is built on empirical testing. Our facilities feature one of the most comprehensive independent electrical testing laboratories in Europe:
Replacing an aging legacy motor (whether built 30, 40, or 50 years ago) often presents severe civil engineering challenges. Our specialized engineering group recreates exact shaft centerlines, foot mounting dimensions, terminal box orientations, and cooler flange configurations. We deliver a true drop-in replacement motor that bolts directly onto your existing bedplate with zero structural modifications required.
Our senior application engineers are ready to assist you with technical specifications, ATEX/IECEx compliance certificates, CAD dimension drawings, and competitive export pricing.
Contact UsTechnical answers to common procurement, compliance, and engineering questions regarding CE certified explosion-proof motors.
Whether you require standard low-voltage Ex d industrial motors or bespoke multi-megawatt high-voltage Ex p rotating machines, our engineering experts deliver tailored solutions with international compliance, verified efficiency, and uncompromising safety.
Contact Us