Explore our heavy-duty industrial electric motors, wound rotor slip ring motors, and specialized stator rewinding components manufactured under ISO 9001 and IECEx quality benchmarks.
In high-voltage (HV) electrical rotating machinery—spanning 3.3kV, 6.6kV, 10kV, and up to 13.8kV induction motors, slip-ring units, and synchronous generators—the stator winding is the structural and electrical heart of the machine. Over decades of severe duty cycles, thermal stress, transient surge voltages, and environmental contamination degrade stator insulation, leading to inter-turn faults, phase-to-ground dielectric breakdown, and catastrophic plant outages.
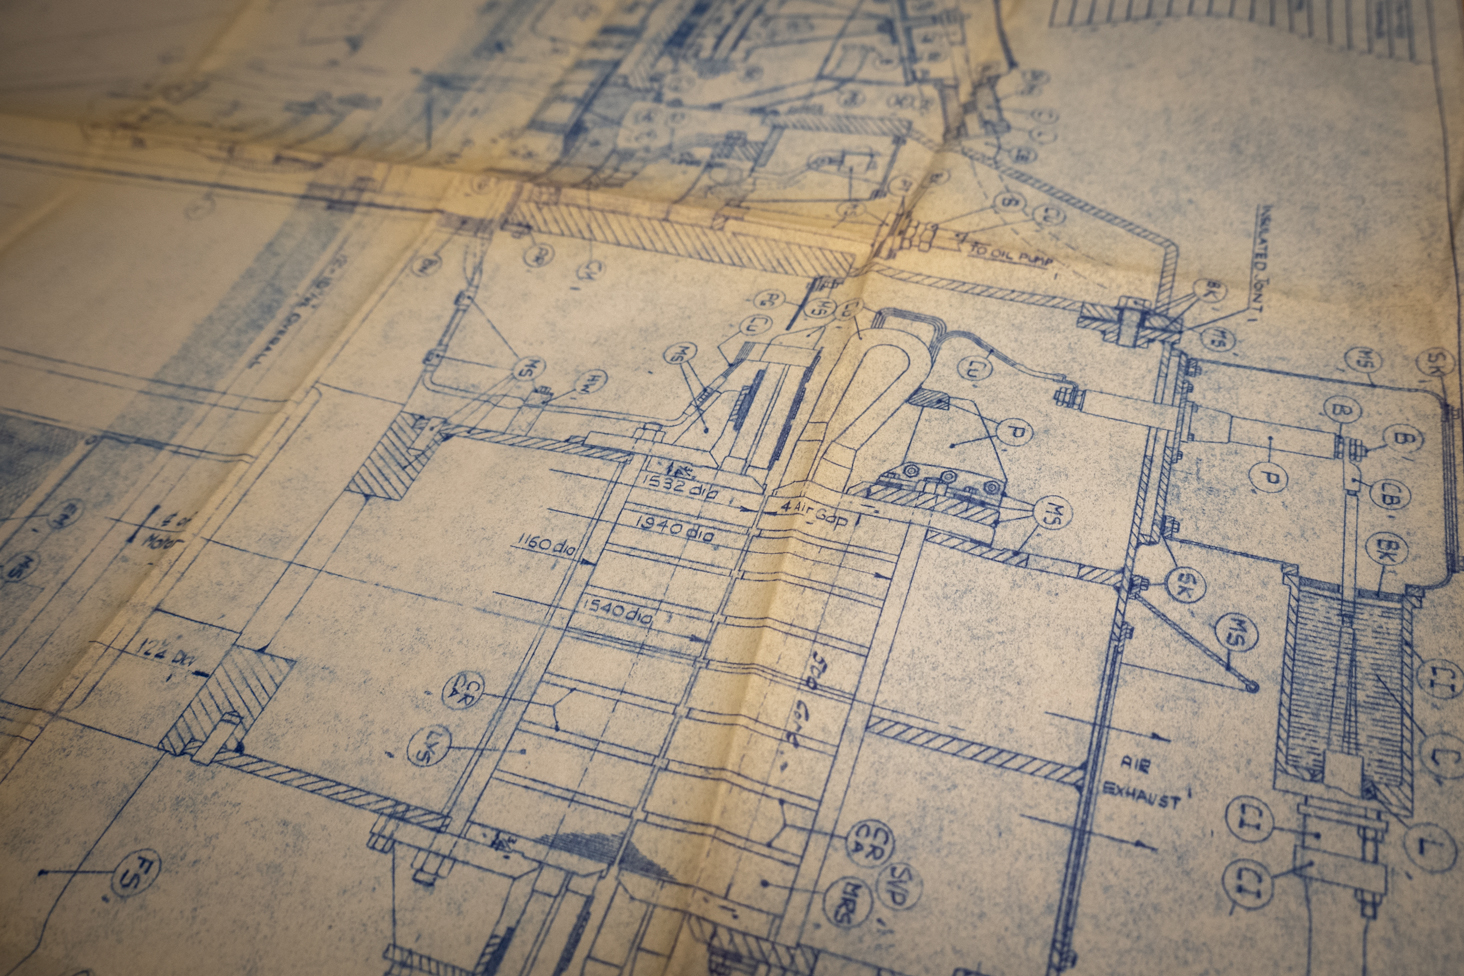
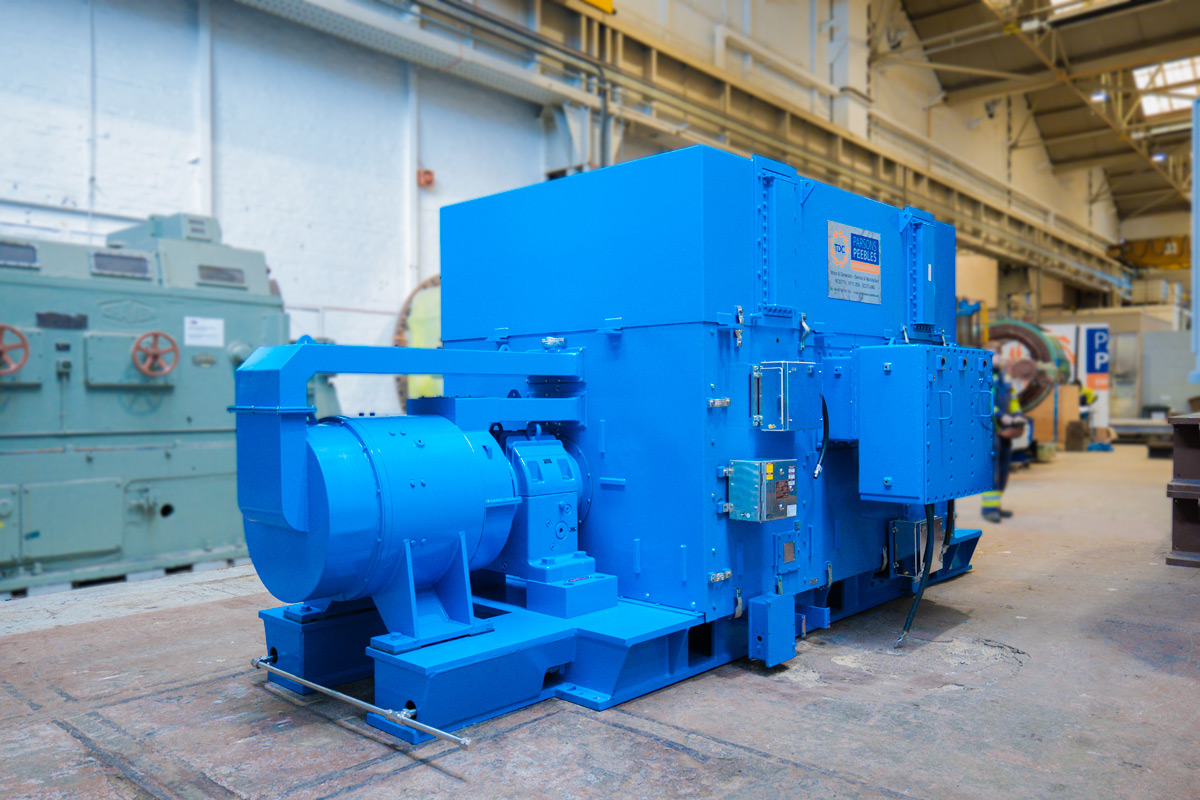
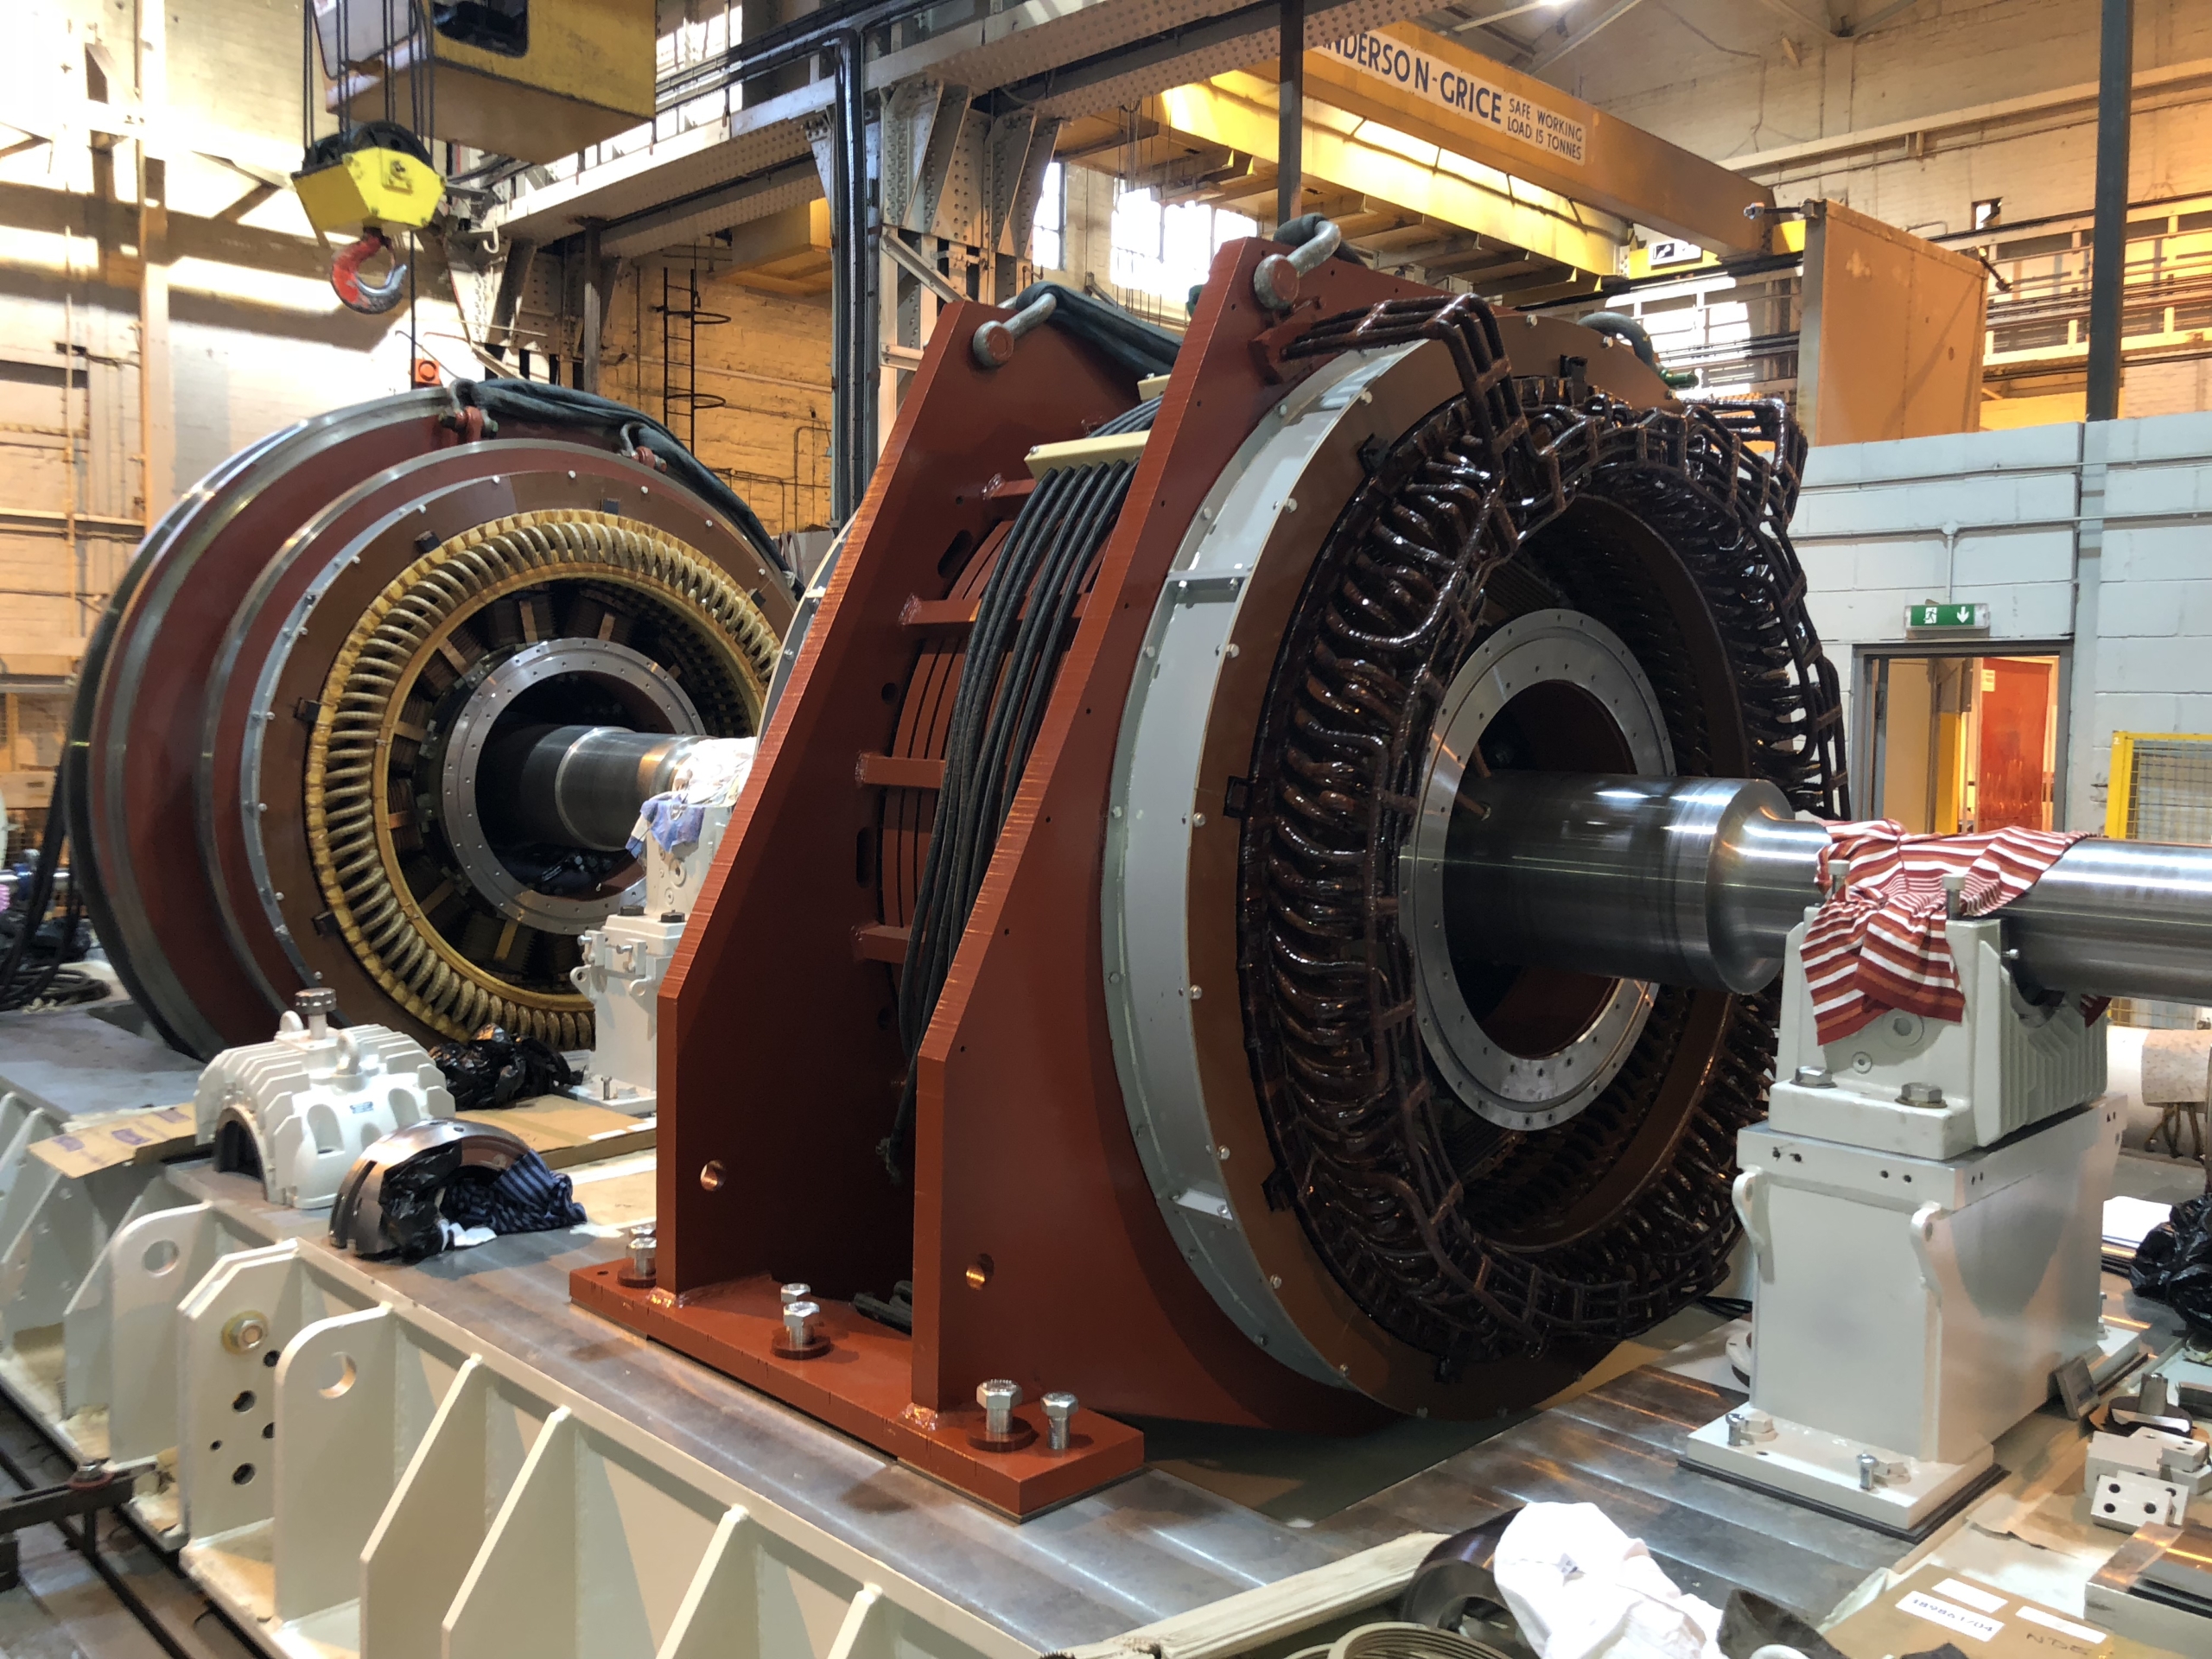
As China’s leading High Voltage Stator Rewinding Manufacturer and specialized OEM factory, we synthesize 128+ years of foundational electromechanical engineering heritage with cutting-edge manufacturing automation. Combining rigorous European engineering standards (inherited through technical collaboration with legacy leaders such as TDC Parsons Peebles) with advanced Chinese supply chain scale, our facility delivers unparalleled precision in stator coil fabrication, vacuum pressure impregnation (VPI), core restoration, and comprehensive high-voltage load testing.
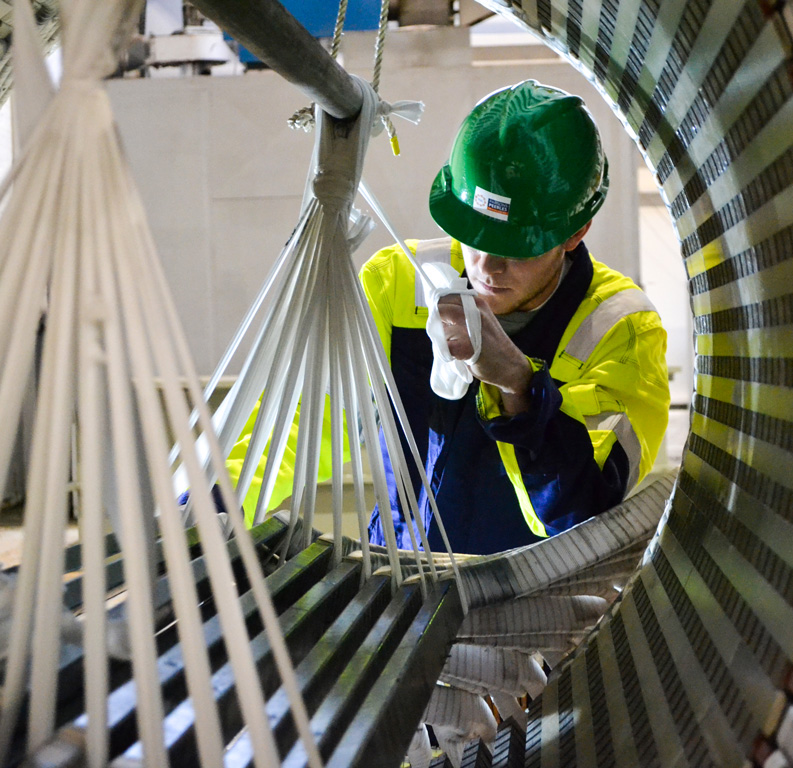
Our 35,000 m² cleanroom manufacturing and overhaul facility is equipped with automated CNC diamond-coil shaping machines, hydraulic coil pressing jigs, automated laser core loss testers, and an advanced 20 MVA high-voltage test center capable of full-load, back-to-back, and partial discharge diagnostics.
Full capability in manufacturing and rewinding ATEX/IECEx certified explosion-proof stators (Ex d, Ex p, Ex ec). Our insulation systems utilize inorganic mica tapes paired with solventless epoxy resins rated for Class H (180°C) continuous operating temperatures.
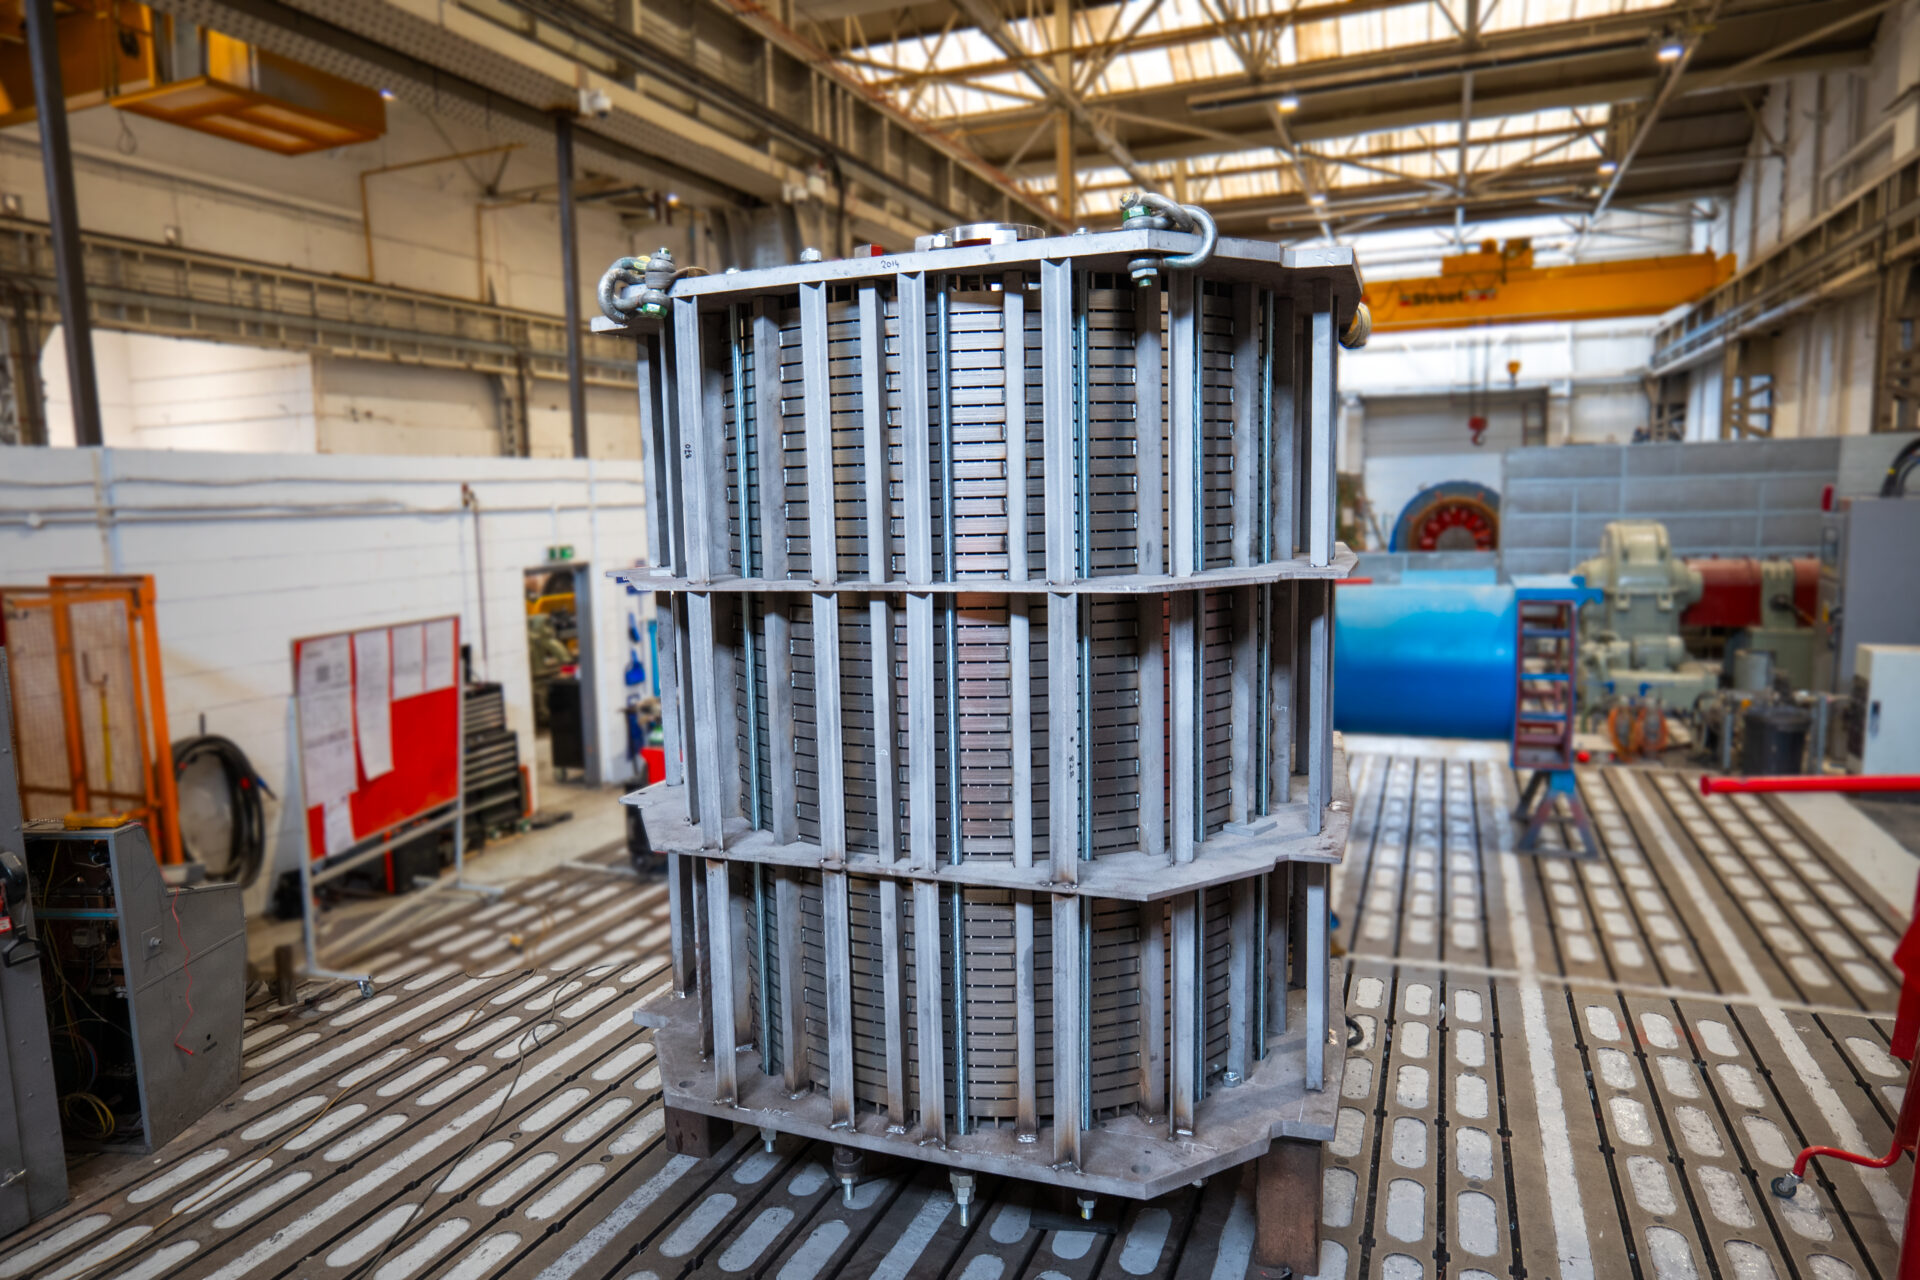
Using 3D optical scanning and electromagnetic modeling, we reverse engineer legacy stators from global manufacturers (WEG, Siemens, ABB, Parsons Peebles, General Electric). We guarantee 100% mechanical drop-in fit without modifying baseplates or couplings.
Integrated anti-corona conductive and semi-conductive grading tapes (SiC embedded) eliminate surface partial discharges up to 13.8kV. Dual-cycle Vacuum Pressure Impregnation ensures zero void formation in slot sections.
Stator rewinding is not merely a repair task; it is a high-precision manufacturing procedure designed to optimize electromagnetic efficiency and eliminate thermal bottlenecks. Below is an engineering overview of our proprietary 7-step stator life-extension process:
| Process Stage | Engineering Methodology | Quality Benchmark & Verification |
|---|---|---|
| 1. Core Stripping & Pyrolysis | Controlled thermal burnout at < 380°C to prevent interlaminar core insulation degradation. Mechanical coil removal. | Core Loss Test (W/kg) & Hot Spot Thermography (< 5°C variation). |
| 2. Core Lamination Restoration | Deburring, re-insulating shorted laminations with organic varnish, keybar torque tightening, and slot cell dressing. | Core Flux Ring Test at 1.5 Tesla induction. Zero hot spots permitted. |
| 3. Form-Wound Coil Fabrication | Oxygen-free high-conductivity copper (OFHC) stranded conductors, insulated with multi-layer porous mica tape. | Turn-to-turn surge test up to 5x nominal operating voltage per IEEE 522. |
| 4. Slot Insertion & Wedge Locking | Precision coil inserting into slots, magnetic or epoxy-glass wedges installed, ripple springs inserted for thermal expansion. | Slot tight fit verification (< 0.05mm clearance) to prevent slot vibration. |
| 5. Corona Shielding Application | Conductive tape applied to slot portion; semi-conductive SiC tape applied to overhang transitions. | Surface resistance mapping (10^3 to 10^9 Ohms/sq) for PD suppression. |
| 6. Vacuum Pressure Impregnation | Full stator submerged under 1 mbar vacuum, followed by 6 bar hydraulic pressure with 100% solid epoxy resin. | Resin viscosity tracking & gel point monitoring per IEC 60034-18-31. |
| 7. Final QA & High Voltage Testing | Comprehensive electrical diagnostic suite performed before customer dispatch. | Dissipation Factor (Tan Delta), Partial Discharge (<100pC), AC Hi-Pot test. |
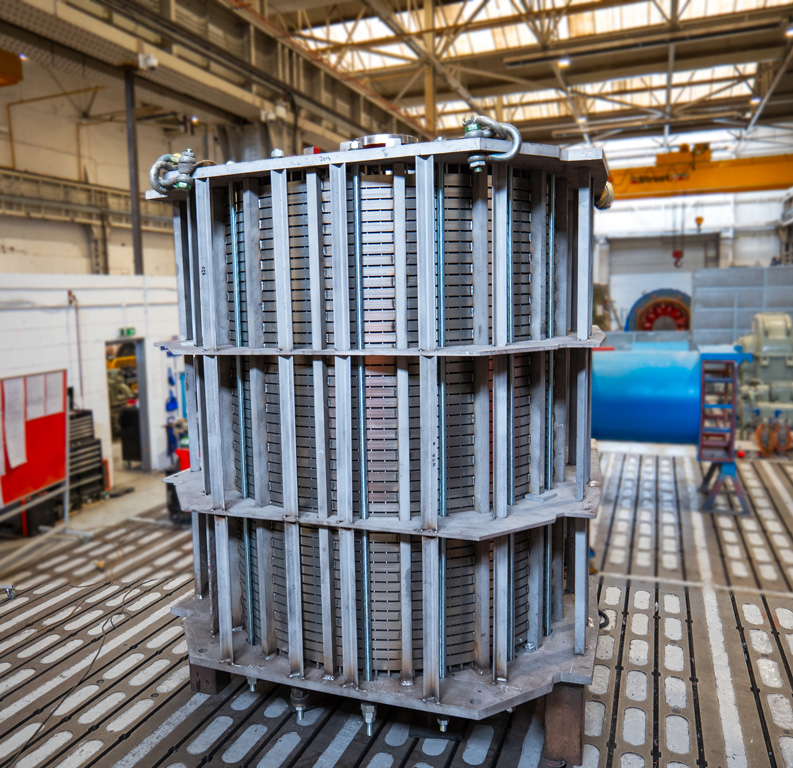
Prior to rewinding, the stator core lamination stack is subjected to high-flux core loss testing. Any inter-laminar shorts cause severe localized heating during motor operation, leading to premature winding failure.
Our engineering team performs full-ring flux testing and infrared thermal imaging to identify and repair damaged lamination packs before installing new coils, guaranteeing optimal efficiency gains.
As global industries accelerate toward decarbonization, continuous operational uptime, and higher power-density machinery, procurement strategies for high-voltage stators are undergoing a fundamental paradigm shift. Asset managers are moving away from reactive "breakdown rewinding" toward strategic OEM life-extension engineering.
Modern global buyers require stators pre-fitted with embedded fiber-optic Distributed Temperature Sensors (DTS) and online Partial Discharge (PD) couplers directly within the slot overhangs. This allows continuous real-time cloud analytics of winding health without stopping production.
With the widespread adoption of High-Voltage Variable Frequency Drives (VFDs), stators face severe steep-fronted voltage transients (dV/dt stress). Future rewinding procurement specifies specialized inverter-duty nanocomposite mica tapes designed to resist corona erosion from high PWM frequencies.
To eliminate extended site downtime during rewinding, major power plants and refineries now procure complete pre-built "drop-in" stator core and frame assemblies. The old stator is swapped out within 48 hours, while the original unit is returned to our factory for refurbishment.
The high-voltage electric motor repair and manufacturing industry is experiencing significant technological breakthroughs. Key development vectors shaping China's export dominance in stator manufacturing include:
Understanding the operational trade-offs between insulation chemistries is crucial for long-term reliability. Our factory offers custom insulation tailored to your environmental conditions:
Here are expert answers to the most common questions raised by industrial procurement directors, plant engineers, and maintenance managers when sourcing stator rewinding services from China:
Complete rewind of a severely damaged 10kV pump stator for a municipal water authority. Upgraded from Class F to Class H VPI insulation, resulting in a 4.2% motor efficiency increase and zero partial discharge activity.
Re-engineering and rewinding a 46-year-old 12 MVA hydro generator stator. Replaced damaged lamination packs, installed anti-corona form-wound coils, and restored unit output to full rated capacity.
Manufactured 4 units of 6.6kV Ex p pressurized induction motor stators for an offshore FPSO vessel. Fully certified under IECEx guidelines with dual-redundant RTD thermal sensors.
Need immediate technical consultation, a fast quote for high voltage stator coil manufacturing, or a complete drop-in stator replacement? Our senior engineering team is available 24/7.