
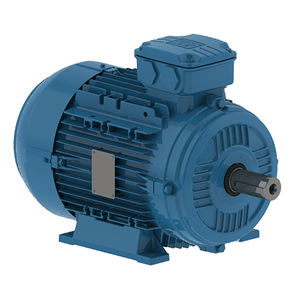
Electric Motor Industrial Fan 15kW 3-Phase Asynchronous Induction Drive
- Rated Power: 15 kW (20 HP)
- Voltage Option: 380V / 460V / 60Hz
- Duty Cycle: S1 Continuous Heavy Duty
- Application: Mine Ventilation & Auxiliary Draft






Our export-grade, heavy-duty three-phase induction and wound rotor (slip ring) AC motors are built to conquer high thermal stress, high starting torque demands, and severe duty operational profiles required by New York mining, tunneling, and industrial operations.
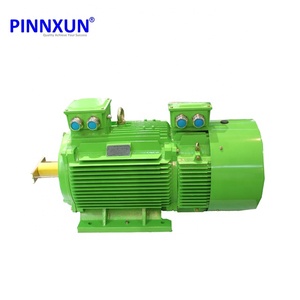
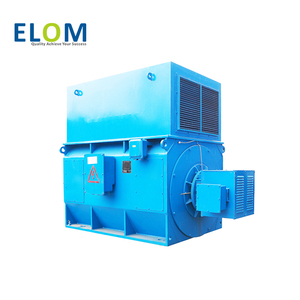
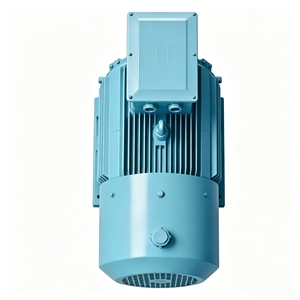
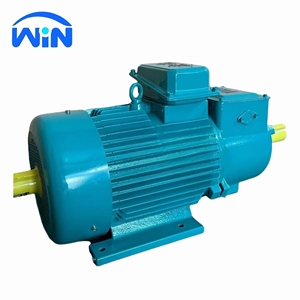
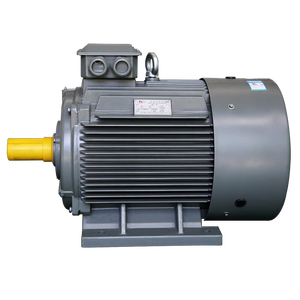
Mine hoist drives represent the most safety-critical rotating electrical assets in underground extraction facilities, deep civil tunneling networks, and heavy industrial aggregate operations. Unlike continuous pump or fan loads, mine hoisting applications involve severe intermittent duty cycles (S3/S4 thermal demands), frequent accelerating and braking phases, extreme thermal dynamics, and high shock loading during cage acceleration and skip loading.
For mining engineers, infrastructure directors, and procurement executives across Upstate New York, the Hudson Valley, and Metropolitan New York City underground civil works, selecting an optimal mine hoist motor factory and export partner requires deep alignment with North American electric utility standards (60 Hz grid frequencies, NEMA MG-1 standards, IEEE 841 severe-duty requirements) as well as rigorous workplace safety compliance mandated by MSHA (Mine Safety and Health Administration) and OSHA.
Wound rotor (slip ring) AC motors provide soft, high-torque starts up to 280% Full Load Torque (FLT) while eliminating violent line-current spikes on suburban NY distribution grids.
Class H mica-tape insulation systems treated with advanced solventless epoxy resin ensure zero moisture ingress, essential for damp underground mine shafts and flooded tunnels.
Custom bedplate adaptation, shaft extension matching, and terminal box repositioning allow complete mechanical interchangeability with legacy GE, Westinghouse, and Reliance motors.
The geological landscape and civil infrastructure of New York present unique operating environments for heavy-duty electric motors. From historical salt and mineral extraction shafts in Upstate New York to massive subterranean transit and water tunnel construction beneath Manhattan, our factory engineers custom heavy-drive solutions tailored to localized site conditions:
Operating in regions like the Finger Lakes and St. Lawrence County, deep rock salt and industrial talc mines demand explosion-resistant (MSHA-certified) slip ring motors. High ambient humidity and corrosive airborne salt ions require stainless steel slip ring assemblies, anti-corrosion marine epoxy coatings, and IP55 total enclosures.
Extensive crushed stone, limestone, and granite quarries supplying the New York construction corridor utilize high-capacity inclined skip hoists and overland conveyors. YZR series heavy wound rotor motors provide exceptional thermal endurance under continuous 150% duty cycles and heavy shock loading during primary crusher dumping.
Major municipal infrastructure initiatives—such as MTA subway expansions and Water Tunnel No. 3 engineering—require heavy vertical muck hoist drives. Operating in restricted urban staging areas, these motors must feature ultra-low acoustic signatures, low electromagnetic interference (EMI), and VFD-compatibility for precise position control.
The industrial procurement landscape in New York State is shifting under stringent regulatory frameworks and grid modernization goals. Buying engineers must evaluate mine hoist motors not only on mechanical horsepower, but on full life-cycle cost, compliance with NY State’s Climate Leadership and Community Protection Act (CLCPA), and compliance with federal workplace safety standards.
To meet NY State energy reduction targets, mine operators are transitioning from inefficient low-voltage motor banks to direct medium/high-voltage AC drives (2300V, 4160V, 6kV). Direct high-voltage connection reduces I²R copper line losses by up to 14% across long cables in deep vertical shafts.
Modern NY mines are adopting proactive predictive maintenance. Our mine hoist motors are shipped pre-instrumented with dual PT100 RTDs per phase, SPM shock pulse bearing monitoring nipples, and tri-axial digital accelerometer mounts for continuous cloud telemetry.
Imported machinery must seamlessly bridge international IEC design standards with North American NEMA MG-1 and IEEE 841 standards. Our factory provides dual-stamped NEMA/IEC nameplates with standard 60Hz winding designs (460V, 575V, 2300V, 4160V) designed specifically for NY grid feeds.
Choosing between standard squirrel cage induction drives and wound rotor (slip ring) motors depends directly on shaft depth, payload mass, grid supply stiffness, and control complexity. The table below outlines core technical parameters engineered by our factory:
| Specification Parameter | YR / YZR Wound Rotor Motors | YE2 / IE3 Squirrel Cage Induction Motors | Direct Drive Synchronous Hoist Motors |
|---|---|---|---|
| Starting Torque Ratio | Up to 280% - 300% Full Load Torque | 160% - 200% Full Load Torque | 200% - 250% Full Load Torque |
| Inrush Current Impact | Low (1.5x - 2.5x FLC with Resistors) | High (6.0x - 8.0x FLC Direct-On-Line) | Low (Controlled via Inverter Drive) |
| Speed Regulation Control | Rotor Resistor Banks / Slip Energy Recovery | Variable Frequency Drive (VFD) Dependent | Closed-Loop Vector Inverter System |
| Thermal Overload Capacity | Exceptional (Extraneous Rotor Losses) | Moderate (Stator Absorbs Rotor Losses) | High (Water/Air Cooled CACW Options) |
| Ideal NY Application | Deep Vertical Shafts & Weak Grid Mines | Auxiliary Slurry Pumps & Fan Draughts | Ultra-Deep Multi-Rope Friction Hoists |
| Capital Investment (CAPEX) | Cost-Effective High Torque Drive | Lowest Base Machine Cost | Highest Initial Capital Investment |
Rooted in a rich 128-year tradition of heavy electrical rotating equipment engineering—drawing from heritage expertise like TDC Parsons Peebles and modern high-voltage manufacturing protocols—our factory stands as a trusted supplier for demanding global industries. We specialize in custom-engineered replacement motors, complete drop-in retrofits, and high-voltage drive systems that keep underground production moving without interruption.
We maintain an extensive archive of legacy motor dimensions (GE, Westinghouse, Allis-Chalmers, Parsons Peebles). We manufacture exact replacement units matching center height, shaft taper/keyways, and hold-down foot dimensions for instantaneous swapping.
Every motor undergoes comprehensive routine and type testing—including No-Load Current testing, Direct Load testing, Vibration Spectrum analysis, High-Potential Dielectric withstand testing, and Partial Discharge verification prior to export containerization.
We provide full-service export packing (heavy-duty ISPM-15 vacuum foil timber crating) with expedited ocean freight direct to the Port of New York & New Jersey, supported by complete customs documentation and duty clearance handling.
Our manufacturing plants operate under internationally audited quality standards, ensuring maximum operational reliability in severe duty applications.
Yes. All motors exported to New York are explicitly wound and dynamically balanced for 60 Hz utility grids (460V, 575V, 2300V, 4160V, or 13,800V). Standard synchronous speeds match 60Hz poles (e.g., 1800 RPM for 4-pole, 1200 RPM for 6-pole, 900 RPM for 8-pole).
Absolutely. We frequently replace legacy General Electric, Westinghouse, Reliance, and Louis Allis hoist motors. Our engineering team replicates foot dimensions, shaft height, diameter, keyways, and terminal box placement to ensure zero site modification is required.
By connecting external variable resistor banks or liquid resistance starters (LRS) to the rotor slip rings, the motor operates at high slip during startup. This generates up to 280% starting torque while maintaining inrush line currents as low as 1.5x to 2.5x Full Load Current.
For hazardous underground applications (such as coal or methane-bearing strata), we provide explosion-proof enclosures certified under ATEX, IECEx, and MSHA 30 CFR Part 18 specifications, equipped with flameproof terminal boxes and pressurized Ex p purge units.
Standard frame sizes (75kW to 315kW) are typically produced within 4 to 6 weeks. Custom high-voltage heavy frame slip ring motors (up to 3200kW+) take 8 to 12 weeks, followed by expedited maritime shipping direct to the Port of New York & New Jersey.
Every heavy hoist motor includes 6x PT100 RTDs embedded within the stator windings (2 per phase) and 2x PT100 RTDs on drive-end and non-drive-end bearings. Space heaters (120V or 240V) are standard to prevent moisture condensation during mine shut-down periods.